
How to Achieve a Perfect Crosscut on Wooden Elements: Expert Tips
A perfectly straight, clean cut on the end of a wooden part is the calling card of a quality product. Whether it is a glued panel, a flooring board or a decorative batten, the accuracy of the crosscut affects not only the appearance but also the strength of the finished structure. Achieving a square cut with no chipping, burrs or saw marks is a task that calls for an understanding of the processes involved, the right tools and a well-honed technique. Mistakes at this stage can lead to gaps in the joints, distortion of the product’s geometry and, ultimately, rejects.
Specialists at woodworking plants face the need to produce thousands of flawless end cuts every day, on a wide variety of wood species. Their accumulated experience has allowed them to develop a system of rules and techniques that guarantee a consistently high result. This is not about some secret technology but about meticulous attention to detail: from the choice of saw blade and the machine setup to the correct feeding of the workpiece and the subsequent treatment of the cut. In this article we take a detailed look at every aspect of professional crosscutting, so that you can put this knowledge into practice and produce products of flawless quality.
Preparing the Tool: The Foundation of Everything
The key to success in any endeavour is quality preparation. In woodworking this rule is of paramount importance. It is impossible to achieve a clean, accurate cut with a blunt or wrongly chosen tool. The leading player in the crosscutting process is the saw blade. Its condition and characteristics have a direct bearing on the end result. Before starting work, the blade must be carefully inspected for chipped teeth, resin build-up or signs of wear. Any defect will affect the quality of the cut.
Choosing a saw blade is a science in its own right. For end cuts, especially when working with hardwoods or coated materials (MFC, veneered panels), you should use blades with a high tooth count (from 60 to 100 or more for a standard diameter of 250–300 mm). The tooth grind also plays an important role. The most suitable for a clean crosscut is considered to be the alternate combination of a flat and a trapezoidal tooth (ATB or TCG). This geometry lets the main tooth make the main cut while the secondary tooth cleans up the edges, preventing chipping.
The saw itself is no less important. Whether it is a mitre saw, a table saw or a panel-sizing centre, the equipment must be precisely set up and calibrated. The main parameter that needs checking is the squareness of the saw blade relative to the table and the fence. A 90-degree angle must be set with the utmost accuracy. High-precision squares are used for checking. Any deviation, even by a fraction of a degree, will result in a skewed cut, which becomes especially noticeable when two parts are joined.
It is also essential to make sure there is no play in the moving parts of the machine. The arbor on which the blade is mounted must not have any run-out. The guides along which the saw unit travels must be clean and provide smooth, straight movement without jerks or binding. Regular cleaning and lubrication of the equipment is a mandatory condition for keeping it in working order and achieving a consistent cut quality. Neglecting these basic procedures inevitably leads to reduced accuracy and a higher percentage of rejects.
Besides the blade and the machine, the auxiliary equipment also matters. A dust-extraction system not only keeps the workplace clean and protects the operator’s health but also improves the quality of the cut. Chips and dust, promptly removed from the cutting zone, do not obstruct the view and do not clog the gullets between the blade’s teeth, which reduces friction and heat. Good lighting of the workplace is likewise an indispensable factor, allowing precise positioning of the workpiece and control of the cutting process.
Finally, before starting production work it is always advisable to make test cuts on offcuts of the same material you will be working with. This lets you verify not only that the machine is set up correctly and the blade is sharp, but also how the particular wood species reacts to processing. Sometimes, even with perfect settings, features of the wood structure — interlocked grain, for example — can cause chipping. A test cut will reveal this in advance and let you adjust your technique.
Setting Up the Mitre Saw: Precision in Every Degree
The mitre saw (or “chop saw”) is one of the most common machines for making accurate crosscuts. However, even an expensive professional tool is rarely perfectly set up “out of the box”. Checking and calibrating all the key angles is a mandatory procedure before starting critical work. The main task is to achieve a perfect 90° angle between the plane of the saw blade and the table, and between the blade and the rear fence. It is precisely these two parameters that ensure a square cut.
To check the squareness of the blade and the table, a reference square is used. The saw unit is lowered to its bottom position, and the square is placed with one side against the table and the other against the side face of the blade (not the teeth). There should be no gap between the square and the blade. If there is, you need to adjust the tilt of the saw using the special screws provided in the design. They are usually located at the base of the tilt mechanism. Once perfect contact is achieved, the setting must be locked.
The next step is setting the 90° angle between the blade and the rear fence. This parameter ensures that the cut is strictly perpendicular to the longitudinal axis of the workpiece. The procedure is similar: the square is placed against the plane of the rear fence and against the side face of the blade. Adjustment is made by turning the saw base until the gap disappears. After this, you need to check whether the pointer on the scale aligns with the “0°” mark. If not, the pointer should also be calibrated.
It is important to remember that the rear fence of a mitre saw often consists of two parts. Both these parts must lie in the same plane. You can check this with a straight batten or ruler. If there is a step between the fence sections, the workpiece will not sit flush and the cut will be inaccurate. Aligning the fences is usually done by loosening the fixing screws and adjusting them.
After setting the main 90° angles, you should also check other frequently used angles, such as 45°. Do not rely entirely on the factory detents. It is also better to check with a precise protractor or bevel gauge. Having set the required angle by the instrument, you can make a test cut on two offcuts and join them together. If the joint produces a perfect right angle, the setting has been done correctly.
Besides the angles, the plane of the cut also affects accuracy. On mitre saws with a slide function, it is important to make sure the blade travels strictly in one plane as it moves back and forth, without deviating to the side. Any play in the guides will result in a cut that is not flat but slightly arched. Eliminating such play is a more complex task, sometimes requiring a trip to a service centre, but without it a quality result is impossible.
During use, settings can drift due to vibration and loads. Regularly checking the calibration — for example, at the start of each work shift — is therefore good practice at any production facility. It takes only a few minutes but helps avoid costly mistakes and guarantees the consistency of the quality of the products, whether they are staircase components, furniture parts or moulded profiles.
Cutting Technique: From Feed to Finish
Even a perfectly set-up tool does not guarantee success if the technique of the operation is wrong. The correct feeding of the workpiece and the movement of the saw unit itself play a decisive role in achieving a clean cut. One of the key points is the feed rate. It should be neither too slow nor too fast. Too slow a feed leads to overheating of the saw blade and the wood, which causes scorch marks on the end. Too fast a feed increases the load on the motor and the blade, which leads to a rough, torn cut and chipping.
The optimal speed is chosen empirically and depends on several factors: the hardness and density of the wood, the thickness of the workpiece and the sharpness of the saw blade. The general rule is: the harder and thicker the material, the slower and smoother the feed should be. The movement of the saw must be confident and continuous. Stopping in the middle of the cut is unacceptable, as it leaves a noticeable step on the cut surface and a mark from the overheating.
When working on a mitre saw, it is important to position and secure the workpiece correctly. It must be pressed firmly against both the table and the rear fence at the same time. Any gap or shift during cutting will result in an inaccurate angle and a poor-quality cut. For reliable clamping, especially when working with short or narrow parts, you should use the built-in clamps that come with most saws. This not only increases accuracy but also ensures the operator’s safety.
Another important aspect of technique is combating chipping. Chips most often form on the exit side of the saw blade, where the teeth “tear out” the wood fibres. There are several professional techniques for minimising this unpleasant effect.
- Using a “zero-clearance insert”. The standard insert in the table of a mitre or table saw has a fairly wide slot for the blade. Replacing it with a homemade insert of plywood or MDF, with minimal clearance around the blade, supports the wood fibres from below, right next to the teeth, and prevents them from splitting out.
- A backing board. When crosscutting a part, you can place a sacrificial board made from a spare offcut underneath it. The saw blade will cut through the main workpiece and enter the backing board, which also prevents chipping on the lower edge. Similarly, by pressing an offcut against the back of the workpiece, you can avoid chipping where the blade exits at the rear.
- A pre-scoring cut. Some machines (panel saws, for example) have a special scoring unit. But you can imitate its action on an ordinary saw too. To do this, make a shallow cut (1–2 mm) in the reverse direction (if the saw’s design allows) or a very slow, shallow cut in the forward direction. This shallow cut scores the top fibres, and the main, deep cut then passes through without chipping.
- Masking tape. Sticking a strip of quality masking tape over the line of the cut also helps hold the fibres and reduce the likelihood of chipping, especially on laminated or veneered surfaces.
When working with long workpieces, you must provide support at the infeed and outfeed of the saw. Using roller stands or special table extensions prevents the material from sagging. A sagging workpiece can “bite” the saw blade or shift during the cut, which is dangerous and is sure to spoil the part. The weight of the workpiece must be distributed evenly across the plane of the machine table.
On completing the cut, it is important not to hurry to raise the saw blade or remove the workpiece. On a mitre saw you should first wait for the blade to stop rotating completely and only then return it to the top position. On a table saw, move the workpiece away from the blade once it has passed completely through. This simple rule helps avoid an accidental touch of the rotating blade against the already-cut end and the formation of a “kickback mark” on it.
Combating Chipping: Preventive Measures
Chipping on the end cut is one of the most common problems, capable of spoiling the appearance of even a perfectly fitted joint. The nature of its occurrence is simple: the saw teeth, moving through the mass of the wood, do not cut but rather chip and break out the last, unsupported fibres as they exit the surface. Brittle wood species, materials with cross-grain (plywood) and laminated or veneered panels are especially prone to this. The professional approach lies not in fighting chips that have already appeared but in creating conditions in which they do not arise.
As already mentioned, one of the most effective methods is the use of backing or “sacrificial” boards. By pressing the part being worked against a flat, dense base, we create support for the exiting fibres. The saw tooth, completing the cut, enters this backing board, and the cut on the main part comes out clean, because the fibres simply have no chance to break off. This method works equally well both for the lower edge of the part (a board on the table) and for the rear one (a board at the rear fence).
Another powerful tool in the fight against chipping is the right saw blade. A blade for crosscutting must have not only a high tooth count but also a special grind geometry. The most common and effective option is blades with an alternate tooth bevel (ATB — Alternate Top Bevel). On such blades, the cutting edge of each tooth is bevelled alternately to the right and to the left. In use, such a tooth enters the material at an angle, as if slicing the fibres rather than chopping them, which significantly reduces the likelihood of chipping.
A more advanced grind is High ATB, where the bevel angle of the cutting edge is even greater (up to 30–40 degrees). Such blades give excellent results on tricky materials like MFC or veneer, producing a cut comparable in quality to sanding. There are also blades with a combination grind, such as TCG (Triple-Chip Grind), where a flat “roughing” tooth is followed by a trapezoidal “finishing” one that cleans up the edges of the cut. The choice of blade must always match the task and the material being worked.
The blade’s rotation speed and the feed rate also affect chip formation. A high spindle rotation speed combined with a smooth, unhurried feed allows each tooth to take a very thin shaving, which minimises the cutting force and reduces the risk of tearing out fibres. It is important to find a balance so as not to allow overheating of the material from too slow a feed either. On machines with variable speed, it is worth choosing the maximum speed for finishing cuts.
Pre-marking the cut line with a utility knife is another effective technique. By cutting through the top layer of fibres or laminate with a sharp blade against a ruler, exactly along the line of the future cut, we create a “groove”. When the saw teeth reach this line, they no longer meet resistance from the top fibres, since those have already been severed. This helps avoid chipping on the visible, most important face of the part. The method calls for care but gives an excellent result.
Nor should we forget about the moisture content of the wood. Wood that is too dry becomes brittle and more prone to chipping. Working with material at its standard moisture content (for joinery this is usually 8–12%) proceeds considerably more easily. If you have to deal with over-dried wood, you should apply all the precautions described above with redoubled attention, use the sharpest blades and the minimum feed rate.
In serial production, to prevent chipping on critical products, panel-sizing saws with a scoring unit are often used. This is a small blade rotating in the opposite direction to the main one, which makes a shallow cut on the underside of the panel immediately before the main blade passes through. In this way the main blade enters material that has already been scored, and chipping on the laminate or veneer is completely ruled out. This is the industry standard of quality for cabinet furniture.
Using Stops and Jigs for Serial Work
When making a batch of identical products, the key parameters become not only quality but also repeatability of dimensions. Crosscutting a large number of parts by hand to a marked line, achieving their absolute identity, is practically impossible. To solve this task, every production facility uses various stops, limiters and jigs. The simplest and most common tool is the end stop (stop block).
Its principle of operation is elementary: a limiter is fixed to the saw base or to an auxiliary fence at a certain distance from the blade. The workpiece butts against this limiter with its end, and then the cut is made. As a result, all the cut parts are of exactly the same length. A simple clamp with a wooden block pressed against it can serve as the stop. The main thing is that the stop be firmly fixed and not shift during work.
To improve convenience and speed of work, there are specialised stop systems. These may be flip stops, which can be quickly moved out of the way if you need to cut a part of a different length without disturbing the main setting. Also popular are systems with a measuring scale stuck along the fence. This allows you to set the stop to the required length without using a tape measure, which significantly speeds up the changeover process.
When crosscutting parts at an angle, for example when making frames, it is important not only to keep the exact length but also to ensure a perfect match of the angles. Here too, stops come to the rescue. For instance, when cutting four parts for a frame, two opposite sides must be of absolutely equal length. Using an end stop, this is easily achieved. It is important to remember that when cutting at an angle, the length of the part is measured along its longest side.
For more complex or curved parts, special templates or jigs are made. A template exactly reproduces the contour or dimensions of the future part. The workpiece is fixed to the template, and then they are worked together on the machine. For example, on a band saw you can cut out a part along the template’s contour, and then bring it to its perfect shape on a router table with a flush-trim bit. In crosscutting, templates can also be used to obtain complex angles or to cut grooves in series.
Using templates makes it possible not only to achieve high repeatability but also to ensure safety when working with small parts. By securing a small workpiece in a larger, easier-to-hold template, the operator can safely bring it up to the saw blade or the router without risking their fingers. This is especially relevant in serial production, where the monotony of operations can dull attention.
When making and using any stops and templates, the main requirement is their rigidity and accuracy. Any play or inaccuracy in the template itself will be reproduced many times over on all the parts made with it. That is why quality, stable materials (top-grade plywood, MDF, aluminium profile) and precise measuring instruments are used to make them.
Ultimately, the use of positioning systems makes it possible to move the process of manufacturing identical parts from the realm of art into the realm of technology. This reduces the demands on the operator’s skill, decreases the likelihood of human error, significantly increases productivity and guarantees a consistently high quality and interchangeability of parts in the finished product, whether it is a batch of window frames, furniture fronts or drawer blanks.
Working with Different Wood Species: Key Features
Wood is a “living” and non-uniform material. Every species has its own unique density, hardness, fibre structure, resin content and tendency to chip. An approach that works perfectly for soft pine may prove utterly unsuitable for hard, dense oak or brittle wenge. A professional always takes the features of the material into account when choosing the tool, the cutting parameters and the working technique.
Softwoods (pine, spruce, lime) are relatively easy to work. They do not blunt the tool as much, but they have another problem — a tendency for the fibres to crush rather than be cut cleanly. When using an insufficiently sharp blade or too fast a feed, the end comes out not smooth but “fuzzy”. For such species it is especially important to use blades with very sharp teeth and to keep an eye on their condition. The feed rate can be higher than for hardwoods.
Hardwoods (oak, beech, ash, maple) call for a different approach. Their high density creates great resistance to cutting. Here the power of the machine and the rigidity of the saw blade’s design come to the fore. The blade must be not only sharp but also strong, with high-quality carbide tips. For such species it is recommended to use blades with a negative or slightly positive tooth angle, which makes the cut more aggressive but also more controllable, preventing the workpiece from being “grabbed”. The feed rate must be moderate and smooth, without jerks.
Exotic and resinous wood species present particular difficulty. Some “exotics” (wenge, for example) are very brittle and prone to splitting along the grain, which calls for the utmost delicacy and the use of every anti-chipping method. Others (merbau, for example) contain a large amount of oily substances that quickly foul the saw blade and cause it to overheat. Resinous softwoods also actively clog the blade with sticky resin. In such cases, regular cleaning of the blade with special compounds is necessary.
Wood-based panels and composite materials deserve separate mention.
- Plywood. Because of its layered structure with the multi-directional grain of the veneers, plywood is very prone to chipping, especially on the top layer. To cut it cleanly you need to use blades with a high tooth count (High ATB), a “zero-clearance insert” and, where possible, backing boards.
- MDF and HDF. These materials are uniform in structure, so chipping on them is less pronounced. However, they are very abrasive and blunt the tool quickly. It is recommended to use blades with special wear-resistant tips for working with them. MDF dust is very fine and airborne, so a powerful extraction system is a mandatory condition.
- MFC and veneered panels. Here the main task is to achieve a clean cut in the decorative coating. Any chip in the laminate or veneer is a reject. The ideal solution is a panel-sizing saw with a scoring blade. In its absence — the use of specialised blades for MFC (High ATB, TCG) in combination with a “zero-clearance insert” and other chip-prevention techniques.
Nor should we forget about such a factor as interlocked grain and the presence of knots. In places where the grain direction changes sharply, the wood behaves unpredictably. Passing through a large, hard knot creates a peak load on the blade and the motor and also increases the risk of chipping at the boundary between the knot and the main mass. When working with such material, you should reduce the feed rate before the problem area to ensure a smooth pass through it.
An understanding of the properties of different materials comes with experience. At a facility that works with a limited range of species, the technical procedures and cutting parameters are worked out down to the smallest detail. But even an experienced craftsman, when faced with a wood species new to them, will always make a few test cuts to assess its behaviour and select the optimal working parameters.
Subsequent Treatment of the End
Even the cleanest cut, made on perfectly set-up equipment, is rarely the finished surface. In most cases the end requires additional, if only minimal, treatment. This is necessary to remove microscopic marks from the saw teeth, to break the sharp edges and to prepare the surface for further finishing (gluing, painting, lacquering). The quality of this final finishing is no less important than the quality of the cut itself.
The first step after crosscutting is chamfering. The sharp edges left by the saw are very vulnerable to mechanical damage. They are easily crushed and chipped during further work with the part or in the use of the finished product. A light chamfer, taken off at a 45-degree angle, significantly increases the durability of the edge. This can be done in several ways: by hand with a fine-grit sanding block, with a special hand edge trimmer, or on a router table with an edge bit.
For top-class products, where a perfect smoothness of the end is required, sanding is used. It is important to understand that the end grain of wood has a structure resembling a bundle of straws. It absorbs moisture and finishing compounds far more actively than the face surface. This feature also shows up in sanding: the end sands more slowly and requires the use of a coarser abrasive at the initial stage. If the face surfaces of the part are sanded, for example, with P120 grit, then for the end you can start with P80 or P100 and then move progressively to finer grades (P150, P180, P220).
It is best to sand ends on stationary machines — a disc or belt sander. This helps preserve the perfect flatness and squareness achieved during sawing. Hand sanding with a random-orbit or orbital sander requires great skill, as it is very easy to “round over” the edges and disturb the geometry of the part. If a hand tool is the only option, you should use a rigid backing and control the process visually and with a square.
If the part is intended for gluing, for example in a glued panel or in a mitre joint, then sanding the ends is not always desirable. Some joiners hold the view that a surface straight from a sharp saw blade or a jointer provides better adhesion for the glue. Sanding can “burnish” the fibres and clog the pores of the wood with dust, which somewhat weakens the glue joint. Here the decision is made depending on the specific task and the glue used.
Particular attention is paid to preparing the ends for painting or lacquering. Because of its high absorbency, the end, after stain or lacquer is applied, will look considerably darker and more matt than the face surfaces. To even out the absorbency, the end must be primed before finishing. For this you can use special pore-filling compounds (sealer primers) or the main lacquer diluted several times over. After the primer dries, the surface is lightly sanded with a fine abrasive to remove the raised grain, and only then is the finishing coat applied.
In some cases, for example when making cutting boards or worktops, the ends require not only sanding but also polishing. By successively using abrasives with grits up to P1000, P2000 and higher, you can achieve a mirror shine on the end cut of hardwoods. Such a surface is not only beautiful but also more hygienic, as it has a minimal number of open pores.
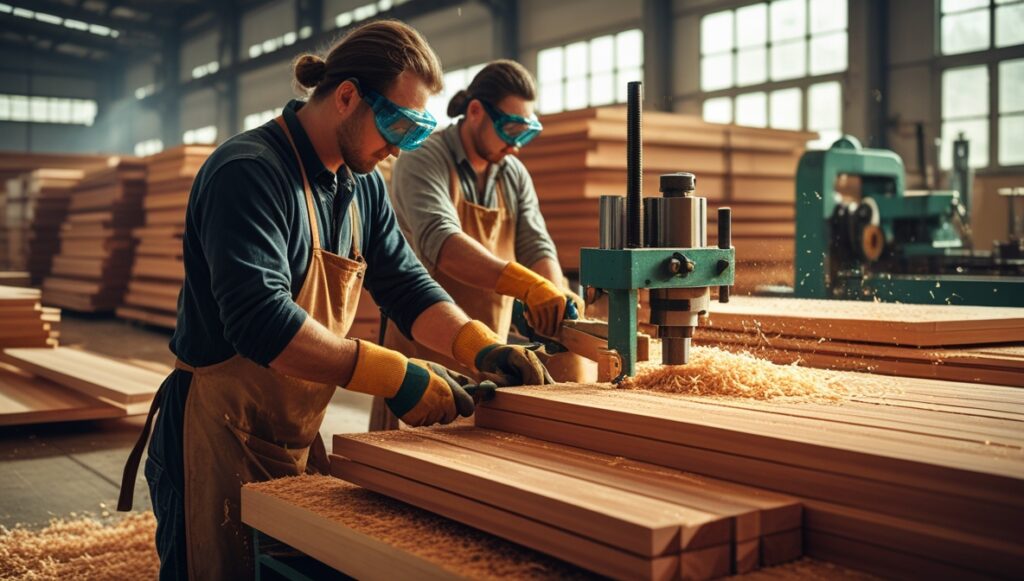
Safety During Work
Any work on woodworking equipment involves an increased risk. The high-speed rotation of the saw blade, the sharp cutting edges and the high power of the machines demand maximum concentration, care and unfailing observance of safety rules from the operator. Neglecting these rules can lead to serious injuries. That is why safety is given top priority at any professional facility.
The first and foremost rule is the use of personal protective equipment (PPE).
- Eye protection. Goggles or a face shield are an absolute necessity. During sawing, fine shavings, sawdust and sometimes even hard particles (an ejected knot or a chipped-off blade tooth, for example) fly off in all directions. Such an object striking the eye can lead to loss of sight.
- Hearing protection. Table and mitre saws produce a high level of noise which, with prolonged exposure, is damaging to hearing. The use of ear muffs or earplugs is mandatory, especially when working throughout a whole shift.
- Respiratory protection. Wood dust, especially from MDF or exotic species, is a strong allergen and carcinogen. The use of a respirator or dust mask helps protect the lungs.
Before switching on the machine, you must always carry out a visual inspection of it. Check that the saw blade is securely fastened, that it is undamaged, and that all the guards are in place. The saw blade guard is not an obstacle but a vital safety element. Removing it is categorically forbidden. It not only protects against accidental contact with the rotating blade but also directs the flow of chips into the extraction system.
The work area around the machine must be clean and well lit. There should be no offcuts, shavings or cables on the floor that you could trip over. A cluttered workplace increases the risk of an accident. The workpiece and all the necessary tools should be positioned so that they can be reached easily, without making sharp or awkward movements.
The operator’s clothing should be comfortable but not too loose. Wide sleeves, flapping shirt tails, ties or jewellery can be caught by the rotating parts of the machine. Long hair should be tucked under a hat. You should work in sturdy, closed footwear that will protect the feet from falling heavy objects.
You should never keep your hands in the immediate vicinity of the saw blade. To feed short or narrow workpieces, push sticks must be used. The distance from your fingers to the blade must always be safe. Do not try to remove offcuts or shavings from the cutting zone while the machine is running. Wait for the blade to stop completely.
Distractions are one of the main enemies of safety. Talking on the phone, listening to music through headphones (unless they are noise-protection ones), chatting with colleagues — all of this reduces concentration. When working at the machine, all your attention must be focused on the operation being performed. If you feel tired or unwell, it is better to break off work.
Before carrying out any adjustments, cleaning or changing the saw blade, the machine must be completely de-energised. Simply pressing the “stop” button is not enough. You must switch off the circuit breaker at the panel or pull the plug from the socket, to rule out the possibility of an accidental start-up of the equipment. Observing these seemingly simple rules helps preserve health and life, allowing you to focus on doing the work well.
Care and Sharpening of Saw Blades
A saw blade is a consumable, but its service life can and should be extended. Proper care and timely sharpening not only save money but also directly affect the quality of the cut and the safety of the work. A blunt blade requires greater effort in feeding, overheats the wood, leaves scorch marks and fuzz on the end, and significantly increases the likelihood of chipping. Working with a blunt tool is a sign of a lack of professionalism.
One of the main problems is the build-up of wood resin, glue and burnt-on deposits on the teeth and body of the blade. This layer increases friction, causes the blade to overheat and reduces the efficiency of its work. The blade starts to cut worse, even if the cutting edges are still fairly sharp. For this reason, regular cleaning is a mandatory procedure. There are special industrial compounds that effectively dissolve resin. In domestic conditions you can use household oven cleaners or concentrated detergent solutions.
The cleaning process is simple: the blade is immersed in the solution for a while (according to the product’s instructions), after which the deposit is easily removed with a brush with non-metal bristles (brass or nylon, for example). The use of steel brushes or abrasives is impermissible, as they can damage the carbide tips or the body of the blade. After cleaning, the blade must be wiped dry and preferably coated with a thin layer of oil to protect it from corrosion.
The signs that it is time to sharpen the blade are: an increase in the effort needed to feed, the appearance of smoke or a burning smell, a deterioration in the cleanliness of the cut, the appearance of “fuzz” on the end. Do not wait until the blade has become completely blunt. Timely sharpening, while the wear of the cutting edge is still minimal, requires removing a smaller layer of metal from the tip, which allows for a greater number of sharpenings and extends the blade’s service life.
Sharpening saw blades with carbide tips is a complex process requiring special equipment. Trying to sharpen such a blade by hand with a file or on an ordinary grinder is a sure way to ruin it. Sharpening is done on special machines with diamond or CBN wheels, which allow the original geometry and angles of each tooth to be restored with high precision.
It is very important that sharpening be done on all faces of the tooth — both the front and the back. Quality sharpening at a specialised workshop makes it possible to restore the cutting properties of the blade practically to factory level. When choosing a workshop, it is worth asking what equipment the sharpening is done on and whether they can work with complex tooth geometries (ATB or TCG, for example).
Saw blades should be stored so as to rule out their contact with one another or with other metal objects. Carbide tips are quite brittle and can chip from knocks. The ideal option is storage in individual packaging or on special racks with dividers, where each blade hangs in its own place.
The service life of a blade is not infinite. After a certain number of sharpenings (usually from 10 to 25, depending on the quality of the blade and the degree of wear), the carbide tip is ground down to such an extent that further sharpening becomes impossible. Such a blade is due for disposal. Economising on the timely replacement of a worn tool always turns into losses in quality and productivity.
Quality Control and Defect Detection
At any production facility, from a small joinery workshop to a large furniture plant, a quality-control system is an integral part of the technological process. The control of the crosscutting of parts is one of the most important stages, since the accuracy of assembly and the appearance of the whole product depend on it. Control should be multi-stage and carried out both by the machine operator and by a specialist from the technical control department.
The first level of control is visual. Immediately after making the cut, the operator should inspect the resulting end. There should be no visible defects on it: chips, burrs, fuzz, scorch marks, steps from the blade stopping. The surface should be smooth and uniform. Particular attention is paid to the visible surfaces and edges that will be on show in the finished product.
The second level is instrumental. Here the geometric parameters are checked. Using a reference square, the squareness of the cut relative to the faces of the workpiece is checked. For this, the square is placed against the wide side of the part and against the machined end. There should be no gap between them. The squareness of the end relative to the edge is checked in the same way.
The length of the part is checked with a tape measure, a calliper or a digital protractor. In serial production, a reference part or a special gauge template can be used for checking. Deviations from the specified dimensions must be within the tolerances stated in the technical documentation for the product. For high-precision joinery products, tolerances can be as fine as tenths of a millimetre.
One of the effective methods of checking the accuracy of an angled crosscut (45° for framed structures, for example) is a “dry” assembly. Two cut parts are joined together. Ideally there should be no gap between them, and the angle they form should be exactly 90°. You can check this with the same square. To check the length of opposite sides of a frame, you simply lay them side by side and compare.
During work the operator should periodically — for example, after every tenth or hundredth part (depending on the batch size) — carry out a full cycle of measurements. This makes it possible to notice in good time if the machine settings have started to drift due to vibration or for other reasons. A defect detected at an early stage makes it possible to avoid producing a large batch of rejected products.
If a defect is nonetheless found, it is important not just to set the rejected part aside but to establish the cause of its appearance.
- Chips: check the sharpness and type of the blade, the presence of a “zero-clearance insert”, the feed rate.
- A non-square angle: check the machine settings (the squareness of the blade to the table and the fence).
- Scorch marks: check the sharpness of the blade, the cleanliness of its surface from resin, reduce the feed rate.
- “Fringe” or fuzz: the blade has gone blunt or is not suited to this wood species.
- A length discrepancy: check the position and fixing of the end stop.
A systematic approach to quality control, keeping statistics on the types of defects and analysing the causes of their occurrence make it possible to continuously improve the technological process, optimise the processing parameters, carry out timely maintenance of the equipment and train the personnel. This is the key to a consistent output of products that meet the very highest standards.





